Food Industry Machinery Manufacturers: Equipment, Types & Selection
Food industry machinery manufacturers play an important role in modern food production by developing equipment for processing.
Modern food processing systems can include automated conveyors, mixers, grinders, filling machines, packaging systems, thermal processing equipment, and inspection technologies. Understanding the different machinery categories can help manufacturers and facility planners identify suitable equipment for specific production requirements.
What Are Food Industry Machinery Manufacturers?
Food industry machinery manufacturers design and produce equipment used throughout food production operations. Their machinery may support individual processing stages or integrate several stages into a complete production line.
Manufacturers commonly develop equipment for industries such as:
- Bakery and confectionery
- Dairy processing
- Meat and poultry processing
- Fruit and vegetable processing
- Beverage production
- Grain and cereal processing
- Snack food manufacturing
- Frozen food production
- Ready-to-eat meals
- Sauce and condiment production
The machinery selected depends on the food product, production volume, processing method, hygiene requirements, and facility layout.
Types of Food Processing Machinery
Food processing machinery manufacturers provide a wide range of equipment. Each machine is designed for a particular stage of production.
Preparation Equipment
Preparation equipment handles the initial treatment of raw ingredients. Common examples include:
- Industrial washing machines
- Vegetable cutters
- Peelers
- Sorting machines
- Slicers
- Crushers
- Grinders
- Destoners
- Ingredient handling systems
These machines can help create uniform raw materials before further processing.
Mixing and Blending Equipment
Mixing systems combine ingredients to achieve consistent composition and texture. Industrial mixers are widely used in bakery, dairy, beverage, sauce, and prepared-food production.
Equipment can include ribbon mixers, paddle mixers, planetary mixers, high-shear mixers, and liquid blending systems.
Thermal Processing Equipment
Heat treatment is used in many food production applications. Depending on the product, facilities may use:
- Industrial ovens
- Steam cookers
- Pasteurization systems
- Sterilization equipment
- Frying systems
- Blanchers
- Dryers
- Heat exchangers
Temperature control is particularly important because excessive or insufficient heating can affect product quality and safety.
Filling and Packaging Machinery
Packaging equipment prepares finished products for storage, distribution, and retail presentation. Common systems include:
- Liquid filling machines
- Powder filling machines
- Pouch packaging machines
- Vacuum packaging systems
- Sealing machines
- Labeling equipment
- Cartoning machines
- Case packing systems
Food packaging machinery manufacturers increasingly integrate automated inspection and control systems into packaging lines.
Food Manufacturing Equipment Comparison
Different machines serve different production requirements. The following table provides a simplified comparison.
| Equipment Category | Primary Function | Common Applications | Automation Potential |
|---|---|---|---|
| Mixers | Combine ingredients | Bakery, sauces, dairy | High |
| Grinders | Reduce particle size | Meat, grains, spices | High |
| Cutters | Size reduction | Vegetables, snacks | High |
| Ovens | Thermal processing | Bakery, prepared foods | High |
| Pasteurizers | Heat treatment | Dairy, beverages | High |
| Fillers | Product dispensing | Beverages, sauces | High |
| Packaging Machines | Product packaging | Snacks, frozen foods | Very High |
| Conveyors | Material movement | Most food plants | Very High |
| Inspection Systems | Quality checking | Packaged foods | Very High |
Industrial Food Processing Equipment Applications
Industrial food processing equipment is adapted to the requirements of different food categories. The same production principle may require different machinery depending on product characteristics.
For example, dairy processing facilities may use pasteurizers, homogenizers, separators, filling systems, and refrigeration equipment. Bakery facilities may require dough mixers, dividers, proofers, ovens, cooling systems, and packaging machinery.
Fruit and vegetable processing may involve washing, sorting, cutting, blanching, drying, freezing, and packaging. Meat processing can involve specialized cutting, grinding, forming, cooking, chilling, and packaging systems.
Automated Food Processing Equipment
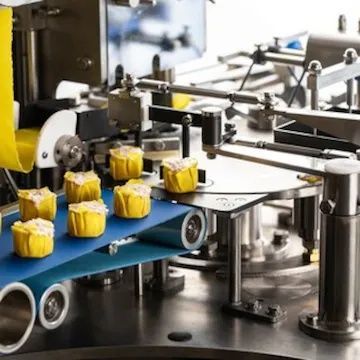
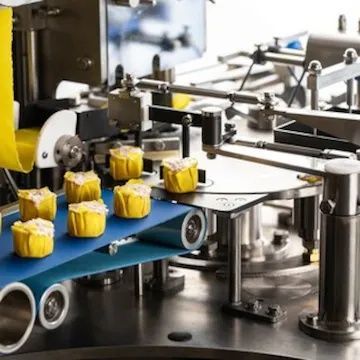
Automation has become an important part of modern food production. Automated food processing equipment can coordinate multiple stages while reducing the amount of manual intervention required for repetitive operations.
Automation may include:
- Programmable logic controllers
- Industrial sensors
- Robotic handling systems
- Automated conveyors
- Machine vision
- Digital temperature monitoring
- Automated filling and dosing
- Production data collection
- Remote equipment monitoring
Connected equipment can also provide production data that helps facility operators identify process variations and maintenance requirements.
Benefits of Automation
Automated systems can provide several operational advantages:
- Consistent processing conditions
- Improved production monitoring
- Reduced repetitive manual tasks
- Better process coordination
- More accurate ingredient dosing
- Faster identification of production abnormalities
- Improved traceability
However, automation should be matched to the production environment rather than implemented without considering product characteristics and operational requirements.
Hygiene and Food Safety Considerations
Hygiene is a central consideration when selecting food manufacturing equipment. Machinery should be designed so that food-contact areas can be inspected, cleaned, and maintained effectively.
Important considerations include:
- Food-contact material selection
- Smooth and accessible surfaces
- Drainage design
- Sealed components where appropriate
- Easy inspection access
- Cleaning procedures
- Corrosion resistance
- Prevention of contamination
- Appropriate equipment separation
Stainless steel is widely used in food-processing environments because of its durability, corrosion resistance, and suitability for many hygienic applications.
Facilities should also consider applicable food safety regulations and sanitary design requirements for their specific region and product category.
Materials Used in Food Processing Machinery
Material selection affects machinery durability, sanitation, and maintenance. Food-processing equipment commonly uses stainless steel for food-contact components and structural areas exposed to moisture.
Other materials may be incorporated for seals, gaskets, belts, insulation, electrical components, and specialized machine parts.
When selecting equipment, manufacturers and facility operators should evaluate:
- Chemical compatibility
- Temperature resistance
- Corrosion resistance
- Mechanical strength
- Cleaning requirements
- Food-contact suitability
- Expected operating environment
The correct material combination depends on the processing conditions and food product.
Energy Efficiency in Food Production Machinery
Energy consumption is an important consideration for large processing facilities. Equipment such as ovens, refrigeration systems, dryers, boilers, and thermal processing systems can represent significant energy loads.
Food processing equipment manufacturers may incorporate efficiency-focused technologies such as variable-speed drives, improved insulation, heat recovery, optimized heating systems, and automated controls.
Facilities can also improve overall efficiency by coordinating production schedules, reducing idle operation, monitoring energy consumption, and maintaining equipment according to manufacturer specifications.
How to Choose Food Industry Machinery Manufacturers
Selecting appropriate food industry machinery manufacturers requires more than comparing individual machines. The manufacturer should understand the production process and the operating environment in which the equipment will be installed.
Evaluate Technical Capabilities
Review the manufacturer's experience with the relevant food category and processing method. Consider whether the company can provide equipment that matches production volume, product characteristics, and required processing conditions.
Review Equipment Specifications
Important specifications may include:
- Production capacity
- Operating temperature
- Machine dimensions
- Electrical requirements
- Material construction
- Automation capabilities
- Cleaning requirements
- Maintenance accessibility
- Control-system compatibility
Consider Production-Line Integration
A single machine must work effectively with other equipment in the production line. Conveyor speeds, product flow, control systems, and machine interfaces should be evaluated before final equipment selection.
Examine Maintenance Requirements
Machinery should be accessible for inspection and routine maintenance. Replacement components, lubrication requirements, cleaning procedures, and maintenance intervals should be clearly documented.
Common Challenges in Food Machinery Selection
Food production facilities can encounter several challenges when planning new equipment.
Space Limitations
Large machines may require significant floor space and appropriate access for maintenance. Facility layouts should account for equipment dimensions, material movement, cleaning zones, and operator access.
Product Variability
Products with different viscosities, moisture levels, particle sizes, or textures may require different processing approaches. Machinery should therefore be evaluated against the specific characteristics of the product.
Integration Complexity
Combining equipment from different manufacturers can create challenges involving controls, communication protocols, conveyor speeds, and production synchronization.
Cleaning Requirements
Equipment that is difficult to access or clean can create operational challenges. Hygienic design should be considered during the planning stage rather than after installation.
Frequently Asked Questions
What do food industry machinery manufacturers produce?
They develop machinery for food preparation, processing, thermal treatment, handling, filling, packaging, inspection, and other production stages.
What is food processing machinery used for?
Food processing machinery is used to transform raw ingredients into finished or semi-finished food products through operations such as cutting, grinding, mixing, heating, cooling, drying, filling, and packaging.
What should manufacturers consider when selecting food production machinery?
Key considerations include production capacity, product characteristics, hygiene requirements, automation, machine materials, facility layout, maintenance, energy use, and compatibility with existing equipment.
Why is automation important in food processing?
Automation can improve process consistency, production monitoring, dosing accuracy, material handling, inspection, and coordination between different production stages.
What materials are commonly used in food processing equipment?
Stainless steel is commonly used for many food-contact and exposed machine components because of its durability, corrosion resistance, and suitability for hygienic environments.
Conclusion
Food industry machinery manufacturers provide equipment that supports nearly every stage of modern food production. Preparation systems, processing machines, thermal equipment, conveyors, filling systems, packaging machinery, and inspection technologies can be combined into production lines suited to specific food products.
When evaluating food processing machinery manufacturers, facilities should look beyond individual machine specifications. Production requirements, hygiene, automation, materials, energy efficiency, maintenance, integration, and facility layout all influence the long-term performance of food manufacturing equipment.
A structured evaluation process can help food producers identify machinery that aligns with their production objectives while supporting consistent processing, effective sanitation, and reliable operation.